Precise small parts · proved before metal

Cut it in the twin. Then cut it for real.

For engineers and labs who need precise small parts the same day, and right the first time. Studio proves any program — from its own CAM, your CAM or your AI — on a physics twin of the MC-1 that runs the machine’s own controller firmware: drives, spindle, cutting forces, chatter, collisions. When the part comes out right in the twin, the same file runs on the same machine.

Windows · Linux · English, Chinese, German, French, Japanese, Spanish · Studio 1.2 · free for learning

MC-1
MC-1 twin
TwinReal

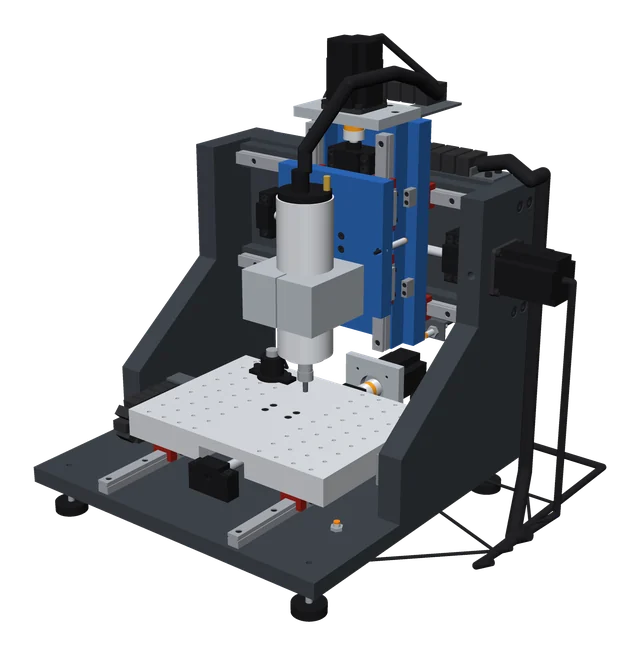
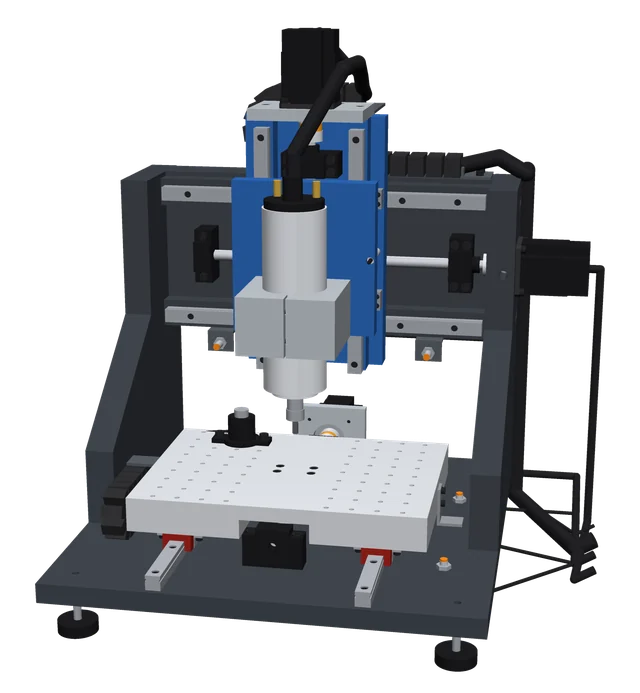
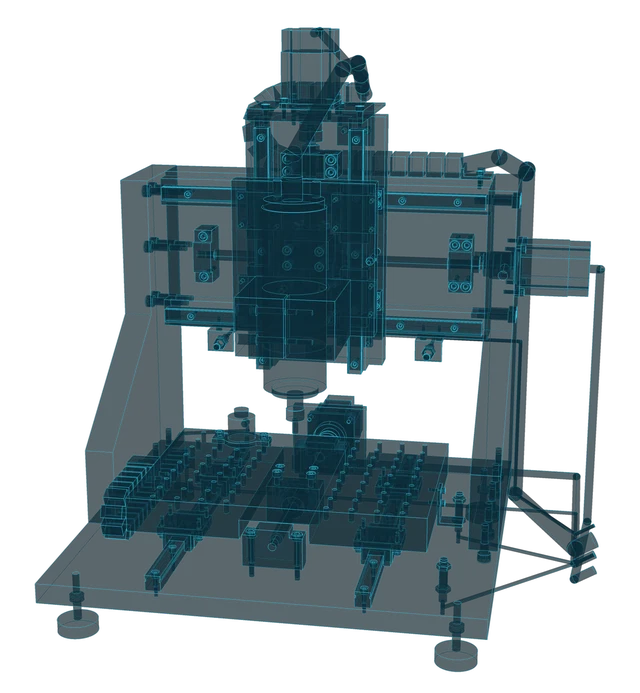
The MC-1 as Studio simulates it (left) and as it is built (right): one model, rendered twice from the CAD.

Own firmwarethe controller code in the MC-1 runs in the twin — and we wrote it
CAM built in2.5-axis and 3-axis toolpaths, cutting data estimated from the twin's physics
422 checksautomated tests on every release, all passing
10 example partsdrawn to ISO, each program run to the end in the twin; more come with updates
Bit-identicalresults on Windows and Linux; every run replays exactly
How it works

Plan and prove in the twin. Make on the machine.

The CAM, the simulator and the mill share one design, one firmware and one set of settings: the program you check in the twin is the program the machine runs, and what the cut does there is the physics model's estimate.

1PLAN

From a drawing to a program

Give Studio a drawing, a mesh, a line of text or a shape your AI describes. Its CAM writes pockets, contours, adaptive clearing or 3D finishing for this machine, with spindle speed, depth and feed set from the twin's physics. Or bring G-code from your own CAM.

In Studio
2VERIFY

Prove the program before metal

The controller's check mode parses every line, and 15 rules catch what it accepts but should not. The run finds rapids into stock, collisions and soft-limit alarms, predicts chatter, compares the part with your CAD, and the optimizer makes it faster without a heavier cut.

In Studio
3MAKE

Cut it on the machine the twin models

The MC-1's controller runs the same firmware with the same settings. Each machine is to be measured at commissioning and its twin set to the measurements, and shadow mode flags the moment the machine and the twin disagree (a preview in 1.0: tested with a second twin standing in for the machine, not yet on a real one).

On the MC-1
Inside the twin

Not an animation of G-code. A model of the machine.

Most simulators draw the toolpath. Studio simulates the controller, the drives, the spindle and the cut, at the timing of the real hardware.

Controller

The machine's own firmware

Twinwright's controller firmware with the MC-1's pin map and settings — the same code the MC-1 ships with. Error and alarm codes come from the firmware itself and are explained in plain language.

Drives

Closed-loop steppers

Following error, pull-out torque and drive alarms; at the higher levels, ball-screw stiffness, backlash and the impacts inside the play.

Spindle

VFD over RS-485

The Huanyang VFD’s Modbus protocol, ramps, load and stall, DC-bus hold-up — and what happens when the cable breaks mid-cut.

Material

Material removal

A height-map workpiece down to 0.01 mm with real tool shapes: flat, ball, bull, V, drill, thread mill, T-slot and dovetail, undercuts included.

Cutting

Forces and chatter

Cutting force and torque for 17 materials, spindle load, tool deflection and stability lobes: Studio suggests a spindle speed its chatter model predicts to be stable, and points out a cut that could break the tool (an estimate).

Accuracy

Errors that real machines have

Lead-screw error tables, straightness, squareness, backlash and thermal growth. Run ISO 230-2 positioning and ISO 230-4 circle tests on the twin.

Electrics

Switches, wires and power

Inductive limit switches, tool setter, E-stop and contactor, power loss and cold start. Inject a broken wire or a glitching sensor and watch how the machine fails.

Workholding

Vises, clamps and tape

Place blanks in a vise, under clamps or on tape, or load your own STL blank. If the cut outgrows the grip, the part slips — as it would.
CAM and programming

CAM that knows the machine.

Studio computes toolpaths for this machine — pockets with islands, contours, adaptive clearing, engraving, 3D roughing and finishing — sets speed, depth and feed from the twin's physics (estimates with nominal parameters), and runs the program to the end in the twin before you see it. Then the editor answers line by line: how long each line took, why a feed was not reached, which rule it breaks.

  • Shapes from SVG, DXF, text, simple shapes or meshes (STL, OBJ, 3MF, glTF) — or described by your AI
  • Speed from the stability lobes; depth limited by chatter, power, grip and tool deflection; feeds tuned in a trial run
  • An editor with per-line times, 15 static rules and breakpoints on force or chatter
  • An optimizer that proves every change in the twin before it keeps it
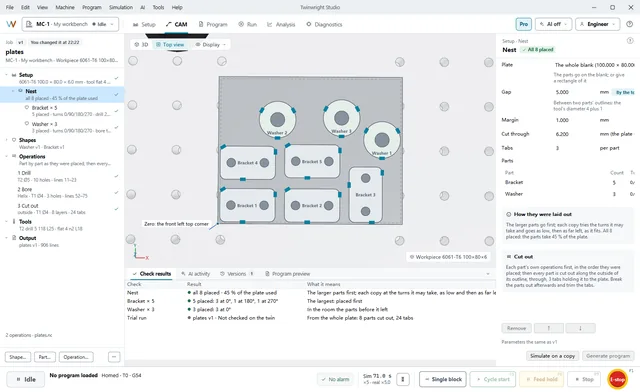
The CAM workspace nesting eight parts on one plate: each placed at the turns it may take, held by tabs, then drilled, bored and cut out in one program.
Studio + AI

Let your AI assistant check its own G-code.

An MCP server is built into Studio. Turn on the AI switch and click Connect: Claude, ChatGPT, Cursor, VS Code or a local model can set up a blank, have Studio's CAM write the program, check, simulate and optimize it, and look at pictures of the result — before anything reaches a real machine.

  • One-click setup for Claude Desktop, ChatGPT desktop, Cursor, VS Code and LM Studio
  • Or chat inside Studio with your own key (Anthropic, OpenAI, DeepSeek, Qwen, Kimi, GLM) or a local model
  • The AI works on twins, never the machine; changes to your window need your OK, and every call is logged
The machine

The MC-1: a small mill built like a big one.

Machined 6061-T6 plates, HGR15 linear rails on every axis, C7 ball screws with fixed and floating end supports, closed-loop steppers and an 800 W water-cooled spindle. 200 × 150 × 80 mm of travel for aluminium, brass and engineering plastics.

200 × 150 × 80 mmtravel X × Y × Z
800 W · 24,000 rpmwater-cooled ER11 spindle
HGR15 · SFU1204 C7rails and ball screws, all axes
~57 kgmachined aluminium frame
Own firmwareon a Teensy 4.1 controller
ISO 230-2measured before it ships

Founders’ batch from $4,990

Indicative prices. USD and EUR exclude VAT or sales tax, duties and shipping; CNY includes 13 % VAT. In the US the MC-1 ships from US stock with the import duty paid: $5,999, the R&D & Lab bundle $9,999.

MC-1
Example parts

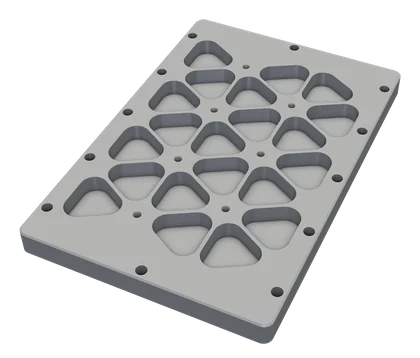
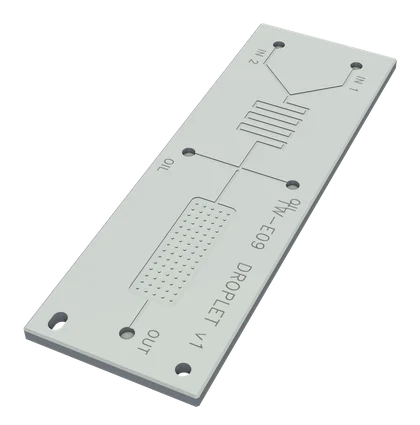
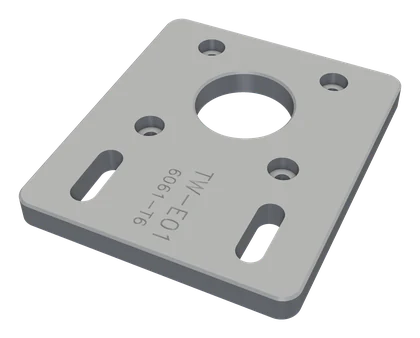
Ten real parts in 1.2, from a motor plate to a watch movement bridge.

Each one is a part an engineer would order — toleranced, drawn to ISO, sized to the standard parts it mates with — and each program is run to the end in the twin and compared with its design.

Evidence

Checked, not just claimed.

Every run replays bit for bit. The example parts and the test results are published with their numbers, and the controller firmware is compared with a reference engine on 26,701 random programs and runs 78 programs from open-source projects. Where a figure is still a design value, we say so.

Start in the twin.

Download Studio — learning is free. Draw a part or load an example, run it in the twin — and when the part comes out right, the same program runs on the MC-1.